Common problems in snus production – and what they really cost

Table of Contents
Snus production is fundamentally a well-controlled and highly automated process. Yet we see time and time again how seemingly small deviations in marking and labeling lead to scrapping, rework, production stoppages and, in the worst case, regulatory consequences.
Here we share real insights from the floor – based on experience from modern snus lines – and go over:
- The most common quality problems
- What they actually depend on
- What is often underestimated
- How to work more proactively
- What is required to future-proof production
As a full-service supplier in industrial labeling, we see this every day.
The most common quality problems at the dose level
1. Incorrectly applied labels
This is by far the most common problem in the industry.
Typical errors:
- Bubbles under the label
- Misplacement in both X and Y directions
- Label applied at an angle
- Not centered against the thumb grip
- Wrong label selected when changing recipe
- Unclear or incorrect batch/code marking
The problem is rarely just aesthetic. Many lines have camera control with fixed tolerances. If the label is crooked or miscentered, the can is sorted out – even if it “looks okay” to the eye.

2. Banner problem
The banner is one of the most demanding applications in the entire snus line. It must not only be applied beautifully – it must seal correctly, align perfectly around a three-dimensional shape, work with perforation, withstand temperature changes and meet regulatory requirements. All of this is done at high speed.
That's why the banner is often the point where small variations have disproportionate consequences.
Common problems:
- Large folds
- Overlap that does not line up
- Cracks in the perforation
- Drop or shrinkage after oven
- Bubbles that only appear after heating

The reasons vary:
- Lid out of tolerance (one side sticks out more than the other)
- Too little glue in overlap
- Material variations in the label
- Temperature influence in the oven
- Chemical properties of the glue
A common scenario: the label looks perfect after application – but after baking, bubbles or shrinkage occur. It is a classic example of a problem that occurs later in the process but actually has its root in material choice and application.
Bundle level problems
When individual cans leave the primary process and are packaged in bundles, the conditions change completely. Now it's no longer about a stable, round unit – but about a composite product where multiple tolerances are stacked on top of each other. This is where many producers underestimate the complexity.
Common problems at the bundle level
- The film does not align with the bundle
- The trunk becomes “twisted” (Turning Torso Syndrome, as we so nicely call it)
- Cans are located at different distances in front
A bundle that is not geometrically correct is difficult to mark correctly in the next step. Instability early in the process spreads further down the line. When the bundle is stable, we know that the process before it is also stable.
And that's where we want our customers to be – with a flow that is predictable, repeatable, and built to last over time.
Problems that are often underestimated
The most underestimated problem is not a single defect – but late discovery.
Example:
- You drive for two hours with the wrong label.
- The recipe has not been updated.
- Parameters are set incorrectly.
- 500–1200 cans must be cleared manually.
The problem is not just the error itself – but the follow-up work that follows. When problems “replace each other”, a domino effect occurs.
Time is the biggest factor. If the error is detected early, it is manageable. If it is detected late, it becomes expensive.
What causes the error?
It is rarely a single factor. Most often it is a combination of:
- Handling
- Material
- Machine
- Settings
- Recipe/programming
Different products require different parameters depending on:
- Material on label
- Speed
- The shape of the can
- Surface texture
Switching between items is a critical point, where many errors occur.
Mechanical fault or adjustment problem?
Distinguishing between mechanical and programming-related errors requires experience – and above all an understanding of how machine, material and logic interact in real time. In practice, this is often where troubleshooting determines how quickly you can get back to stable production.
Example of setup problems:
The product passes the sensor. The machine should feed the label after 3 seconds – but consistently does so after 5 seconds.
→ Clear parameter or programming deviation.
This is a classic example of a setup problem when the product passes a sensor and the machine is supposed to feed the label after three seconds – but consistently does so after five. The delay is exactly the same every time. There is no variation. No “jumping”. Nothing random. It is repeatable, which almost always points to a parameter deviation, incorrect recipe, or a changed time setting in the PLC or labeling system. The machine does exactly what it is told to do – just not what we think it should do.
This type of error is fundamentally logical. It follows a pattern. Therefore, it can also be corrected quickly if you know where to look.
Mechanical or material-related problems behave differently. That's where variation is key. If the label ends up at the leading edge one time and at the trailing edge the next time, without anything being changed in the recipe, it indicates instability in the flow. It could be a sensor that sometimes reads too late due to reflections or dirt. It could be variation in the friction of the adhesive against the can. It could be microscopic differences in can diameter. It could be a conveyor that is not maintaining a constant speed. It could even be vibrations.
Example of mechanical/material-related problem:
The label sometimes ends up at the front, sometimes at the back.
→ Erratic behavior indicates sensor problems, adhesive variation, or mechanical instability.
Ultimately, it's about creating machines and systems that minimize the room for interpretation. Clear alarms, locked parameters and predefined recipes reduce the risk of setting errors. Stable mechanics, the right choice of materials and proper maintenance reduce physical variations.
When you manage to combine both parts, you get a line that is both technically stable and easy to understand. And that's where real operational reliability arises.
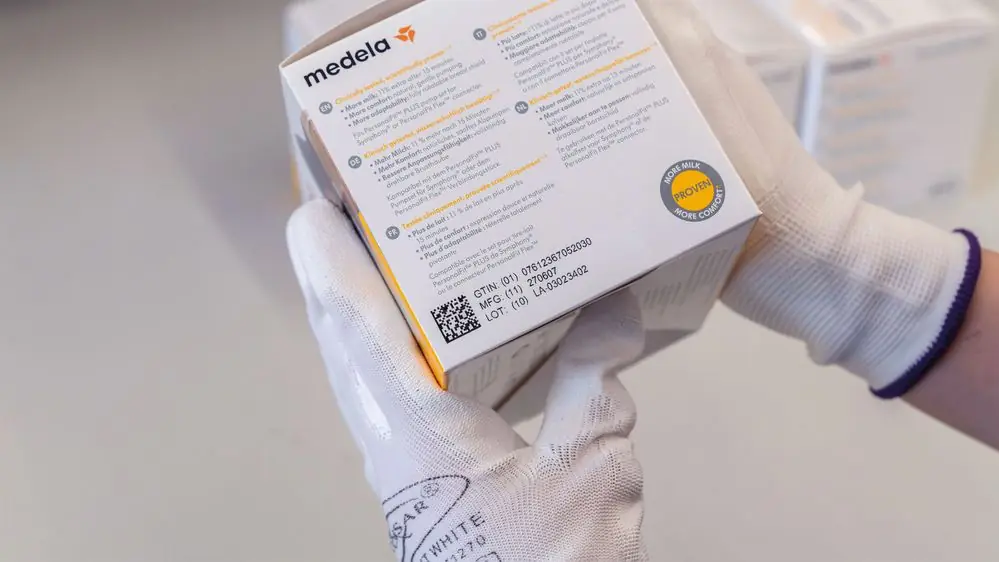
Unreadable batch and date codes
Batch and date coding is perhaps the least visible part of the labeling – but this is not about aesthetics, but about traceability, legal requirements and product safety. A code may be small in size, but the consequences of it being unreadable are large.

Common causes of unreadable codes:
- Insufficient cleaning of printer
- Wrong combination of material and ink/laser
- Too dense text (characters blend together)
- Incorrect setting in the program
A concrete and common problem occurs when numbers merge. A camera can then read two characters as one. For example, a “1” and an “8” can be perceived as an unclear symbol or a single character. This creates immediate traceability problems. The system may register the correct number of characters, but the content is wrong. In the worst case, a miscoded product slips through.

The risks are significant. A can with an unreadable code must not be sent to the market. If it does, the producer could face fines and regulatory action. But the biggest risk is often trademark damageLack of traceability signals a lack of control.
A can with an unreadable code must not be shipped. If it is shipped anyway, the producer risks:
- Fine
- Regulatory measures
- Trademark damage
Traceability is non-negotiable.
How do new can formats affect production?
When a new can is launched, the focus is often on marketing, design and in-store differentiation. But in production, a seemingly small change can have much greater consequences than expected.
It could be a change from a matte label to a shiny, gold variant. From a marketing perspective, it's a visual upgrade. In the machine, it's a whole new reality. Reflections change, sensors lose their reference and suddenly the label is not read correctly. What previously worked stably begins to give errors or stop.

A changed diameter is another classic. A few millimeters can be enough to:
- Index wheel no longer fits
- Controls go wrong
- The application is uneven.
- Conveyor belt not keeping product centered correctly
If you go even further, for example to a hexagonal can, the whole premise changes. Round geometry is predictable in rotation, application and transportation. A hexagon introduces flat surfaces, corners, and new points of contact. It affects:
- How the product rotates
- How pressure is applied
- How sensors read position
- How the can behaves in transport chutes
A new height or changed edge design can also create problems in transitions between machines. Where there were previously margins, jams suddenly arise. Gutters and downspouts that have worked for years are starting to create blockages.
The consequences are often extensive:
- Sensors cannot read the material correctly
- Index wheel must be replaced or remanufactured
- Machine paths and guides need to be adjusted
- Shrink and label stations require new settings
- Production speed must be reduced initially
It is not uncommon for suppliers to be informed late in the process – sometimes when the new product is already in production. In this case, the adaptation takes place during operation, resulting in scrapping and disruptions.
Experience shows us that approximately one in ten producers works structured with tests, verification and technical review before launch. They involve their machine suppliers early and run test series. The result is a controlled start-up.
The others launch first and solve the problems later. It is a significantly more expensive route. Not only in direct conversion costs, but in lost production, stress in the organization and risk of quality deviations.
A new mold is not just a design issue. It is a technical project that affects the entire line – from the first feed to the last pallet. When changes are managed proactively, they become an opportunity. When they are managed reactively, they become a cost.
And in a highly automated snus production predictability is always cheaper than improvisation.
Operator dependency – the biggest factor
If we were to point to an area with the greatest potential for improvement in many snus lines, it is not about replacing technology. Snus production is a complex environment. High speeds, frequent article changes and multiple shifts require clear routines and shared understanding.
That's why adherence to routines is so crucial. When maintenance schedules are followed consistently, when cleaning is done according to plan, and when recipes are always checked when changing items, stability is created. Small deviations in everyday life can otherwise quickly have an effect on production – especially over multiple shifts.
The handover between shifts is another important factor. A clear structure for documentation and communication reduces the risk of misunderstandings and unnecessary adjustments. Stable production is a teamwork where everyone contributes to the whole.
Training is essential, especially when installing new equipment. It's not just about showing how to start and stop the machine, but also about creating an understanding of how parameters, materials and speed interact. When the operator feels confident in the system, quality and efficiency also increase.
At the same time, the machines must be designed with reality in mind. In modern production environments, not be dependent on individual specialistsThe equipment should be intuitive, robust and built to minimize the risk of error.
Incorrect loading of labels shall be mechanically prevented. Critical parameters shall be locked or access controlled. The interface should be clear and informative.

The goal is simple but ambitious: anyone, regardless of background or previous experience, should be able to operate the machine safely and confidently after the right introduction. This creates flexibility for the employer and security for the operator.
That's where the industry is moving – towards more user-friendly technology, clearer recipe control and smarter automation that supports people. When the right training is combined with well-thought-out machine design, you don't just get a stable line – you get sustainable production over time. And that's where real efficiency arises.
Can machines let through defective cans?
Yes – it does happen that defective cans are allowed through production. However, it is important to understand that it is rarely a matter of the machine itself “not working”, but rather how the system is set up and used in the current environment.
What we have seen from various producers is that the problems often arise in the interaction between humans, systems and tolerance settings.
Common causes can be:
- That reference images have been updated in connection with material or article changes
- That a visa or camera program has been retrained without verifying the entire tolerance picture
- That acceptance levels have been adjusted to reduce discarding – but without fully analyzing the consequences
The system is only as good as the settings allow – and that applies regardless of the supplier. When parameters are correctly set and locked, and when changes are made in a controlled manner, modern vision and control systems are very reliable.
What do the problems really cost?
If we calculate conservatively and look at a fully realistic situation in snus production:
500 cans per hour in scrapping.
Approximately 10 SEK in coverage per can.
-> This corresponds to 5,000 SEK per hour.
For an eight-hour shift, it's 40 SEK.
In a week with recurring problems, we end up with around 320,000 SEK.
And then we have only counted on direct scrapping.
We have not taken into account:
- Rework where staff manually remove labels or re-sort batches
- Production stoppage while troubleshooting and adjusting
- Extra staffing or technical support
- Reduced line speed to “drive safely”
- Impact on delivery accuracy
- Brand risk in the event of quality deviations

The biggest hidden cost is rarely the scrapping itself. It is instability. Operators are forced to spend time fine-tuning instead of producing. Small stops break the rhythm. Temporary solutions become permanent. Speed is deliberately kept lower than it should be, “just in case.”
The biggest hidden cost is instability. A line that is constantly being adjusted never reaches its true capacity.
Premium Line vs Unstable Line
In short, based on our experience, we see a clear difference between stable premium lines and lines that constantly struggle with variations.
A stable premium line:
- Run the same article stably
- Has predictable format changes
- Following maintenance schedule
- Has trained operators
- Has optimized flow
There is a clear structure here. Machines, materials and working methods work together. The result is high availability, low scrap and production that delivers according to plan.
An unstable line however, is often characterized by the opposite:
- Constantly adjusted
- Changing article without structure
- Has a lack of handover between shifts
- Focuses on purchase price rather than overall economics
A cheap machine that on paper “does the same job” can in practice become the most expensive solution over time, when you factor in scrapping, downtime, extra resources and lost capacity.
If you, the reader, recognize parts of the description of an unstable line, you are far from alone. The good news is that it is possible to change. With the right analysis, the right structure and the right technical solution, stability can be built up step by step.
What should producers start doing tomorrow?
- Check your equipment
- Identify bottlenecks
- Ensure that procedures are followed
- Invest in education
- Optimize the flow – not just individual machines
It's not about changing everything. It's about creating stability. At Logimark, we work every day to simplify complex labeling, reduce operator dependency, and build lines that not only meet today's demands – but also tomorrow's product launches, new formats, and new materials.
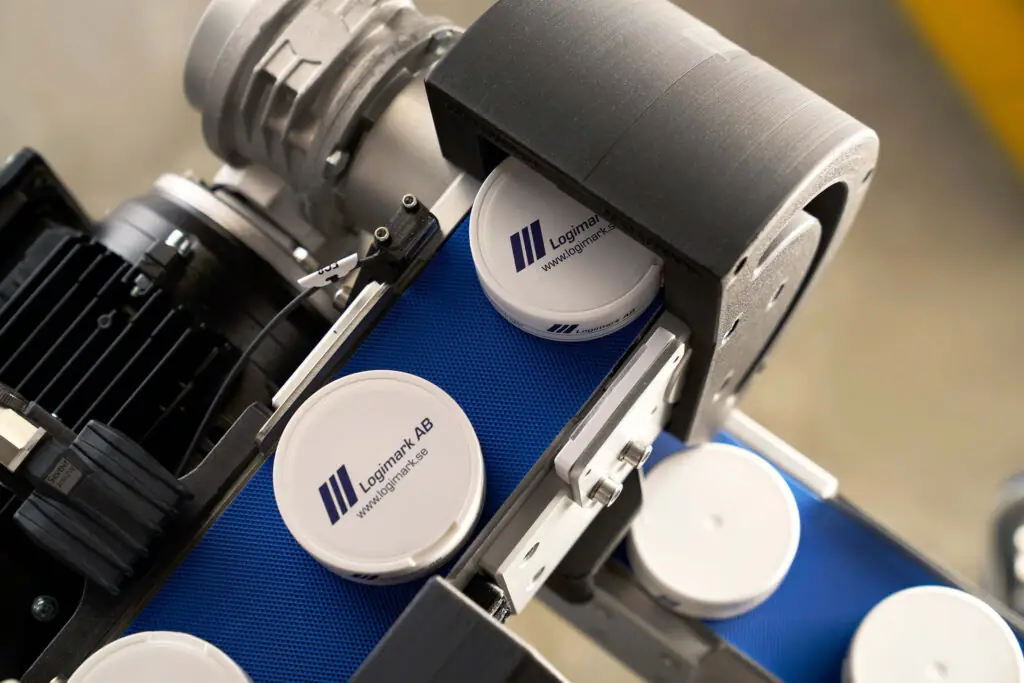

We don't believe in fire department calls as the default mode. We believe in stability as the default. Technology should work for you – not the other way around.
And if your line right now requires more patience than it should, then maybe it's time to raise the bar. We are happy to help you take the step from “it works” to “it flows”.