Labeling in the pharmaceutical industry – when every detail has to be right
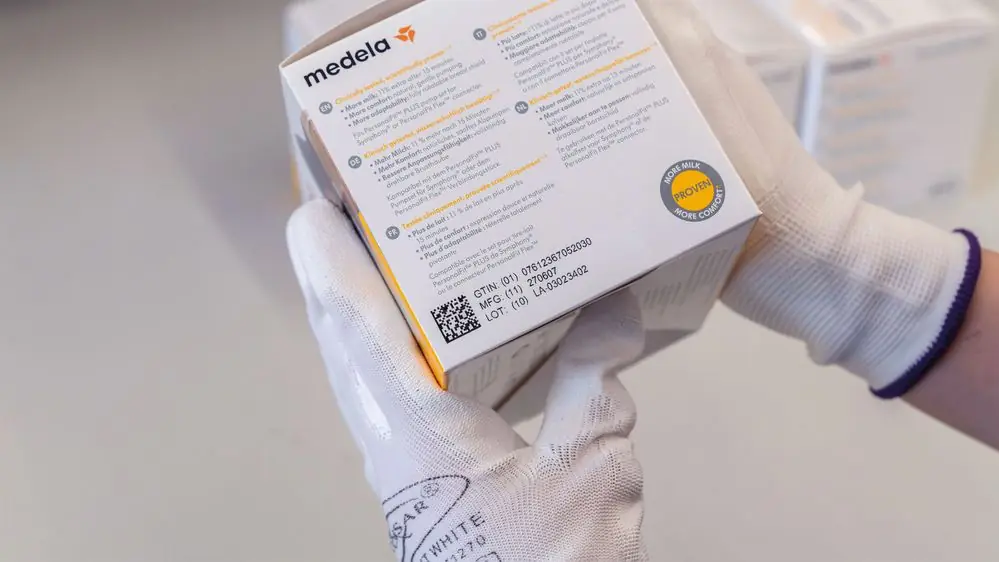
Table of Contents
When we talk about industrial labeling, many people think of a batch number, a best-before date or a label with product information. In the pharmaceutical industry, the reality is much more complex. Here, labeling is an integral part of the product's quality, safety and traceability – and ultimately also part of patient safety.
A misprinted date, a hard-to-read Datamatrix code or a label that comes off can have consequences far beyond the individual product. It can mean production stops, costly recalls, regulatory deviations or, in the worst case, a medicine cannot be identified or verified when it is to be used.
That’s why the pharmaceutical industry places some of the highest demands on industrial labeling. The requirements cover not just the printout itself, but the entire process – from how the information is generated and verified to how it is documented, controlled and archived.
This guide delves into how modern pharmaceutical labeling works. We take a closer look at the technical challenges, different labeling techniques, vision cameras, verification systems, serialization, and how automated labeling solutions contribute to safer and more efficient production.
Drug labeling is about much more than printing a batch number.
In many industries, labeling is primarily used to identify a product or provide the customer with certain information. In the pharmaceutical industry, labeling has a significantly greater function.
Every label is an information carrier that must be traceable throughout the product's entire life cycle. As soon as the product is manufactured, links are created between production orders, batch numbers, serial numbers and other product data. The information then follows the product through filling, labeling, packaging, distribution and finally all the way to the pharmacy.
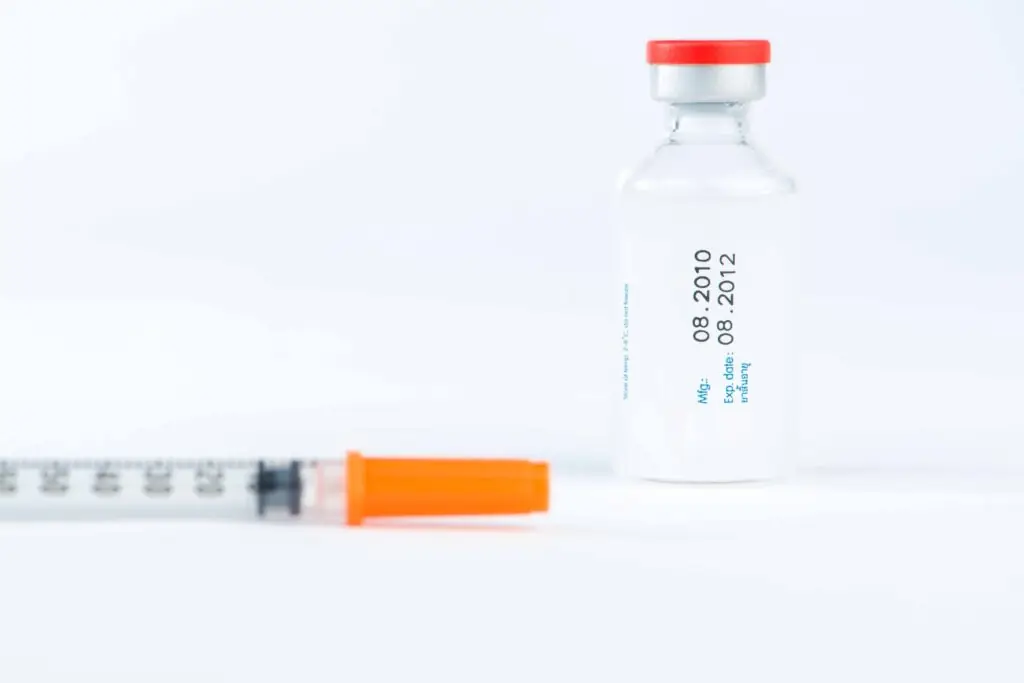
This traceability is crucial if a drug needs to be recalled, if a quality deviation is discovered, or if an authority wants to follow a specific product back to manufacturing.
Labeling therefore becomes a central part of the quality system rather than a final step before the product leaves the factory.
That is why such high demands are placed on the labeling
A label in the pharmaceutical industry must meet significantly more requirements than just being legible.
It should be:
- corrector
- verifiable
- traceable
- durable
- consistently placed
- machine-readable
- documented
In addition, the label must remain legible throughout the product's life. Depending on the type of medicine, the label may need to withstand:
- sterilization
- disinfectant
- UV light
- high humidity
- very low temperatures
- chemicals
- long storage
For example, some laboratory products are stored at temperatures down to -80 ° C, while other products are subjected to sterilization processes where both label material and ink must maintain their properties.
So it's not enough for the label to look good when the product leaves the production line. It must still be fully legible several months or years later.
Government requirements drive development
An important reason for the high requirements is that the pharmaceutical industry is one of the world's most regulated industries.
Manufacturers need to comply with extensive regulations and standards, including: Good Manufacturing Practice (GMP), EU Falsified Medicines Directive (FMD) and GS1 standards plays a central role.
What these regulations have in common is that they aim to ensure:
- that the right medicine reaches the right patient
- that counterfeit medicines can be detected
- that products can be quickly recalled if necessary
- that each product can be identified throughout the entire distribution chain
This means that marking is no longer a stand-alone function. It is part of a larger digital information flow where printers, PLCs, vision cameras, databases and business systems interact.
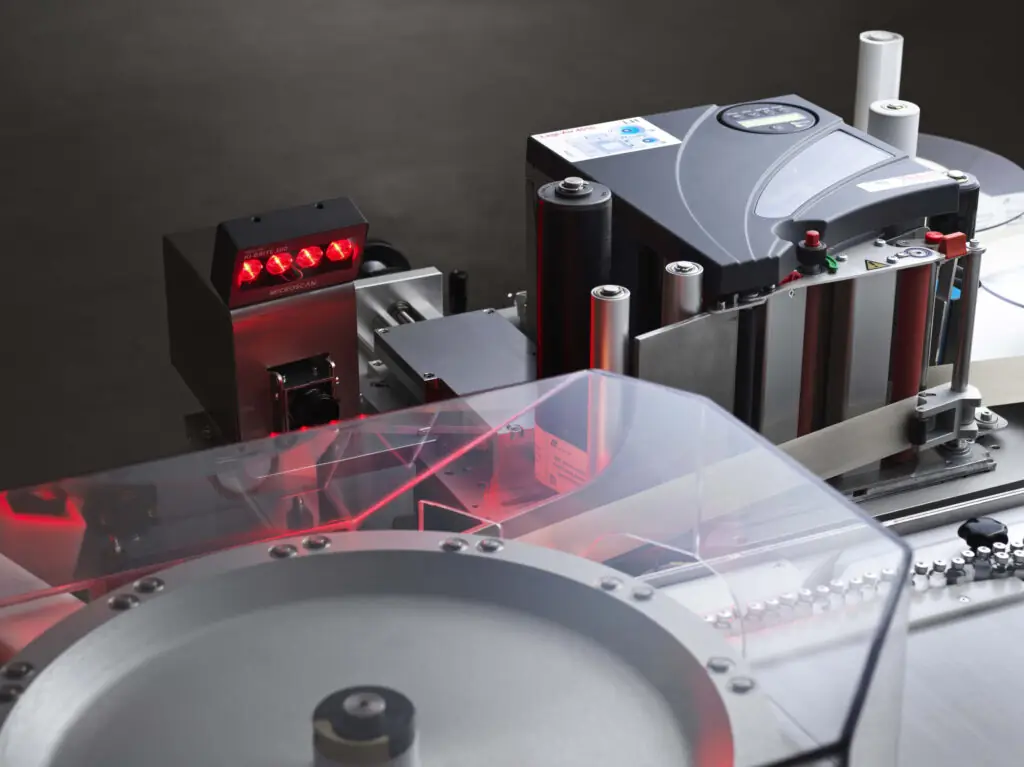
It's not just about writing correctly – it's about proving that it was correct.
A common misconception is that a camera only checks that there is a code on the product. This is rarely the case in the pharmaceutical industry. Instead, modern labeling systems work with multiple levels of control.
First, it is ensured that the right product is in the right place in the production line. Then, it is checked that the correct information is sent to the printer. Once the label is applied, the vision camera verifies that the information was indeed printed correctly.
But the control doesn't end there.
In many production lines, the printed information is also compared with a higher-level system. The camera doesn't just check that there is a serial number – it verifies that it is exactly the serial number the system expected.
It is an important safety feature.
If the operator accidentally selects the wrong product or recipe, it is not enough for the camera to see a fully readable code. It must also be able to detect that the code contains incorrect information.
It is precisely this type of redundancy that makes the pharmaceutical industry's labeling systems significantly more advanced than many other industrial solutions.
Human error should not be able to cause mislabeled products
A recurring principle in pharmaceutical production is that as few steps as possible should be dependent on the human factor.
This does not mean that the operator is unimportant – quite the opposite – but critical moments are built up with multiple levels of security.
When changing recipes or product changes, it is common for two people to need to check and approve the correct product information before production can start.
In addition, at some facilities, every change is documented very carefully.
This may mean that labels, sample prints and inspection reports are saved as part of the production documentation. In some cases, multiple people sign that a label or sample has been discarded or that the correct marking is used before the line is restarted.
It may seem extensive, but the purpose is simple: to ensure that incorrect information never reaches the market.
High production speed makes the challenge even greater
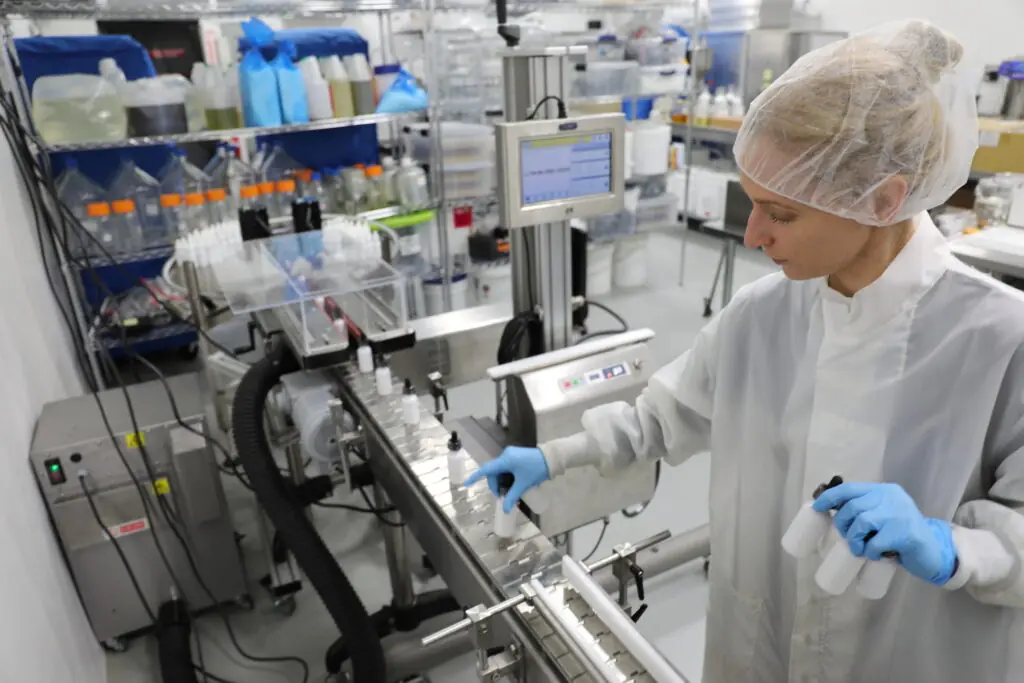
Another factor that makes pharmaceutical labeling technically demanding is the production speed. Small products such as vials, ampoules or injection vials are often produced at very high rates.
It is not uncommon for a filling machine to produce up to 200 products per minute, which is over three products every second. At these speeds, a fast printer is not enough. The entire production line must be perfectly synchronized.
Products must be separated by the correct distance, transported stably through the marking, pass vision cameras, possibly labeled and then collected again - without the products tipping over, rotating or colliding with each other.
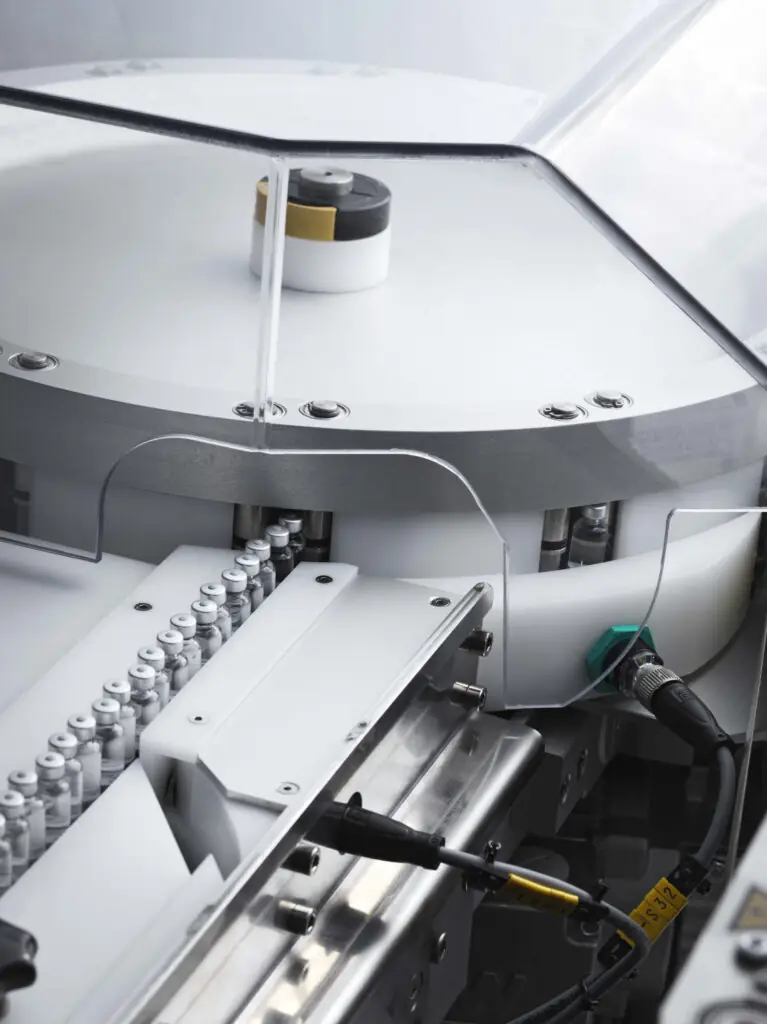
For small cylindrical products such as glass vials and ampoules, this becomes a particular challenge. The products have low weight, small contact surface and can be easily affected by vibrations or changes in speed. In practice, many projects are therefore at least as much about the product flow as the labeling itself.
The shape of the product often determines the entire solution
When discussing labeling systems, it's easy to focus on the printer or labeling machine. In reality, it's almost always the product that dictates how the solution must be designed.
Is the product conical?
Is it cylindrical?
Does it have flat surfaces?
Is it transparent?
Does it reflect light?
Is it coming from the previous machine, standing or lying down?
All of these factors influence the choice of conveyors, controls, sensors, writing technology and vision cameras. In some cases, the product may even need to be oriented or turned before labeling can be performed. This means that two seemingly identical pharmaceutical products may in practice require completely different labeling solutions.
That's why most successful labeling projects don't start with the choice of printer – but with a careful analysis of the product, the material and the production flow.
The choice of marking technology – why there is no universal solution
One of the most common questions we receive is which labeling technology is best for the pharmaceutical industry.
The answer is almost always the same: dIt depends on the product.
There is no technology that is best in all situations. On the contrary, it is the interaction between the product's material, shape, production speed, amount of information and quality requirements that determines which solution will be most reliable.
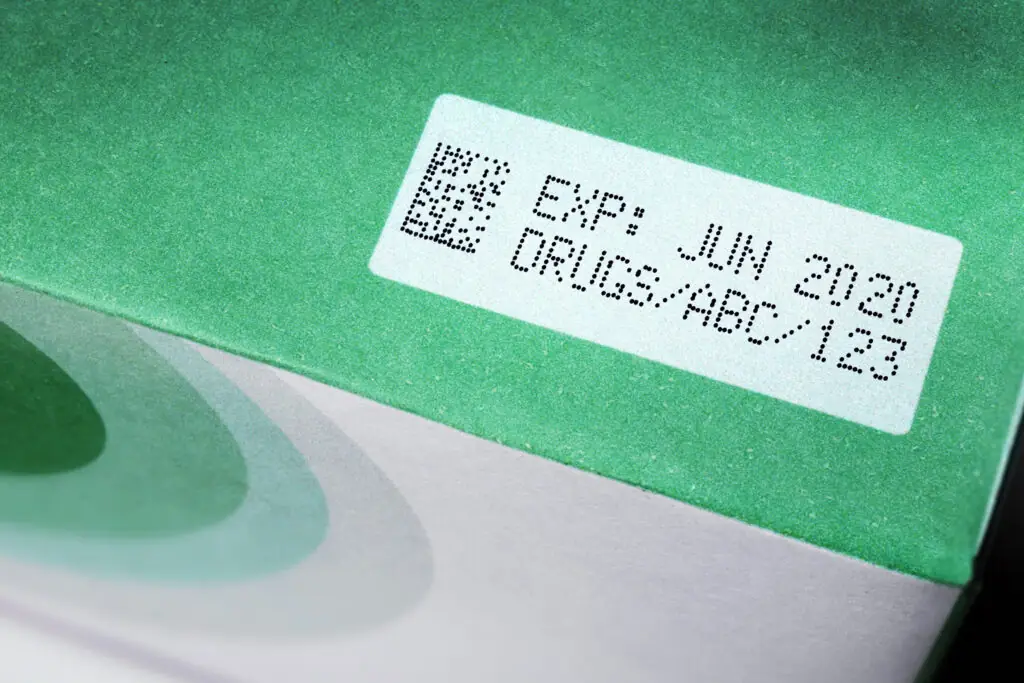
A carton with a Datamatrix code has completely different requirements than a glass vial that passes through the production line at over 200 products per minute. Similarly, a label with very small text requires a different technology than a shipping carton where only a batch number is to be written.
The goal is therefore not to choose the most advanced technology, but the technology that provides the highest operational reliability, best print quality and lowest total cost over time.
Thermal Inkjet (TIJ) – the first choice when print quality is crucial
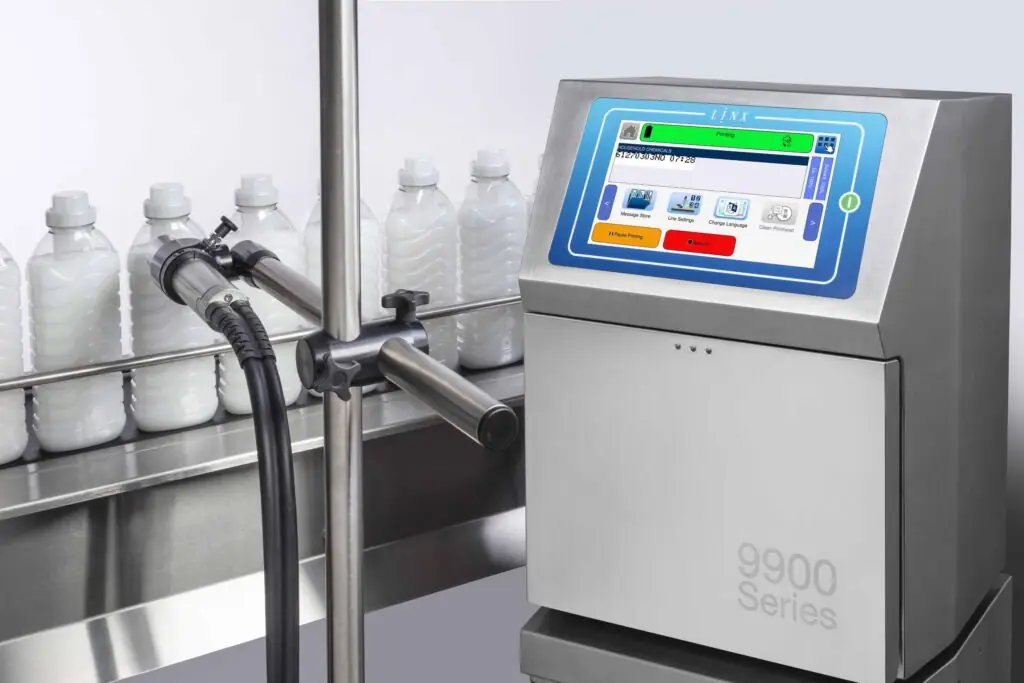
When pharmaceutical companies need to label secondary packaging, such as cartons, Thermal Inkjet (TIJ) often the natural choice. The main reason is the high resolution.
The pharmaceutical industry makes extensive use of Datamatrix codes, small barcodes and very small text. Batch numbers, serial numbers, expiry dates and product information often need to fit together in a limited space, while every detail must be razor sharp.
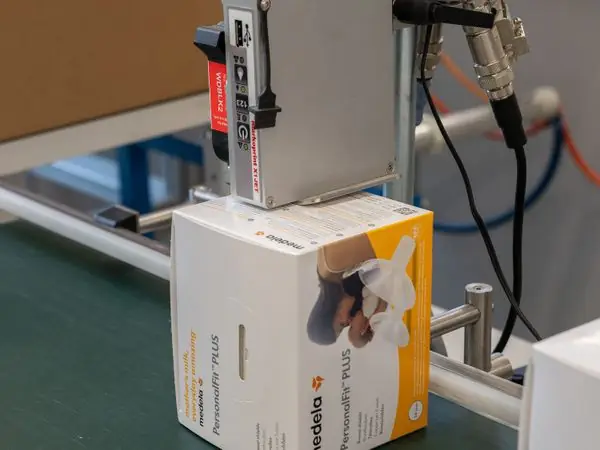
Here TIJ has a big advantage.
The high print resolution makes it possible to print very small characters with high contrast, which is a prerequisite for vision cameras and verification systems to be able to read the information without problems.
It's not just about making the text look good. If a Datamatrix code has too low contrast or if an individual module becomes unclear, the entire code risks being rejected during verification.
Why TIJ dominates carton marking
Another reason why TIJ has become so common in the pharmaceutical industry is the cartridge principle itself. When a cartridge begins to approach the end of its life, it is simply replaced. This means that the print head is also replaced at the same time, which means that print quality is maintained at a consistent level over time.
For a pharmaceutical manufacturer, this is a big advantage. You don't want to risk the print quality gradually deteriorating before anyone notices. Instead, it ensures consistent labeling throughout the entire production run. Although cartridges represent an ongoing consumable cost, the high and stable print quality often outweighs the cartridge cost itself.
In the pharmaceutical industry, product quality is almost always more important than minimizing consumption costs.
The material plays a bigger role than many people think
Cardboard used in the pharmaceutical industry is generally of very high and consistent quality. The surface is smooth, homogeneous and designed to give a good print result. This means that TIJ can deliver very sharp prints with high contrast.
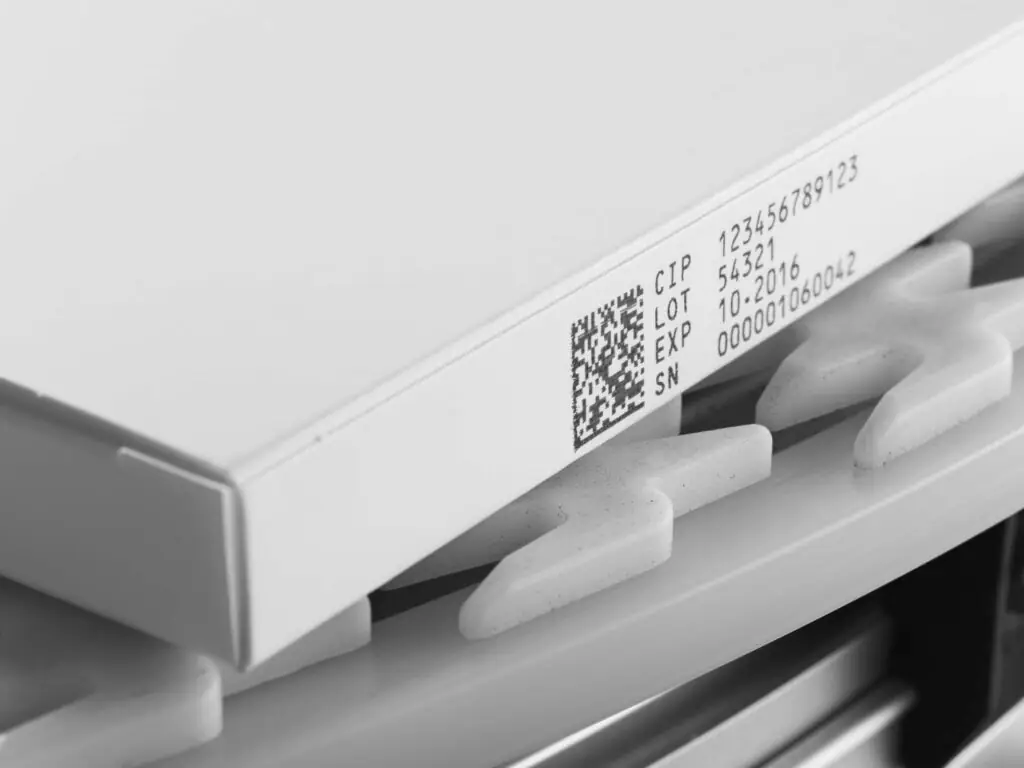
In many other industries, the situation is different. They sometimes use simpler cardboard materials with a coarser surface texture, which can affect how the ink droplets are absorbed and thus degrade print quality.
The pharmaceutical industry, on the other hand, often has higher demands on the packaging material itself, which means that the material is rarely the limiting factor.
Continuous Inkjet (CIJ) – when the production line demands more than resolution
There is a perception that inkjet printer CIJ is being replaced by other technologies. That is not true.
CIJ is still one of the most widely used marking techniques in industry and also plays a very important role in pharmaceutical production.
The difference is that the technology is used where its properties are best used.
When the distance varies
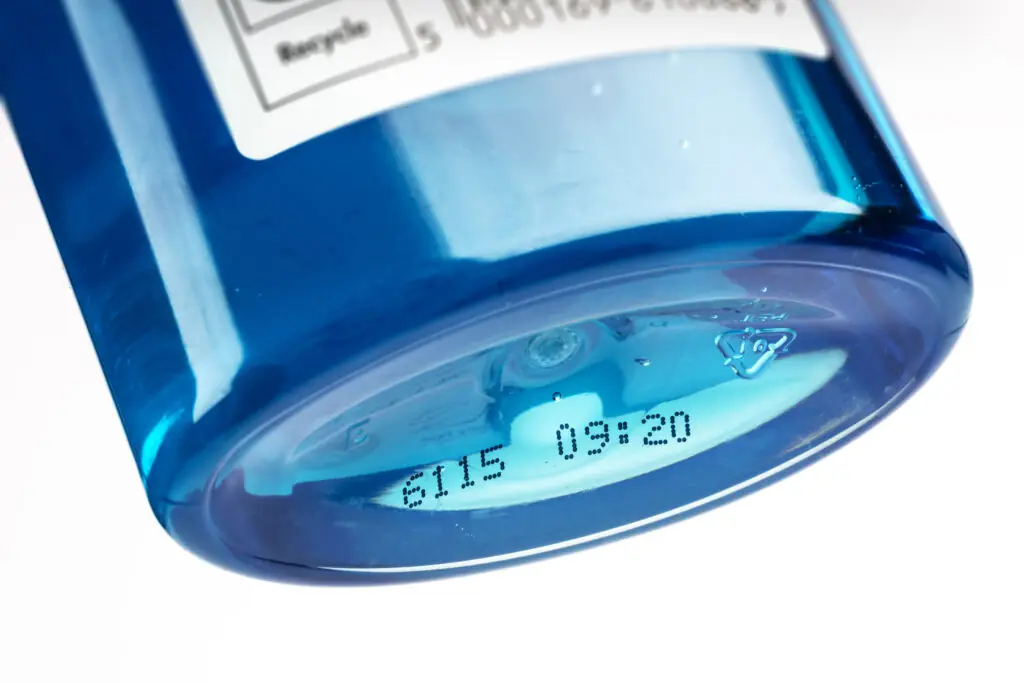
A major advantage of CIJ is that the technology is much more forgiving when the distance between the print head and the product varies. On a production line, it is not always possible to maintain exactly the same print distance. Products can have different heights. Conveyor belts can vibrate. Containers can be uneven.
CIJ works very well here because the inkjet can handle greater variations than, for example, a cartridge-based printer.
This makes the technology particularly suitable for, for example:
- glass bottle
- plastic bottles
- bulbs
- vials
- test tube
- outer packaging
When speed is more important than resolution
There are many applications where the highest resolution is not crucial.
If the label mainly consists of:
- batch number
- production date
- expiration date
- simple barcodes
CIJ can be a very good alternative. Especially on production lines where very large volumes are produced. The technology is developed for continuous operation and can handle high production speeds for a long time.
For many pharmaceutical manufacturers, this represents a very cost-effective solution when the resolution requirements are not as extreme as with Datamatrix codes on secondary packaging.
CIJ is not worse – just different
It's easy to compare resolution between different technologies. But in practice, the choice is rarely about which printer can print the least text. It's about choosing the right tool for the right task.
If the marking is only to identify a shipping box or outer packaging, there is rarely a need for the high resolution that TIJ offers. Instead, CIJ can provide lower operating costs, high availability and very good operational reliability.
Thermal transfer (TTO) – when the label sets the highest standards
Many pharmaceutical products are not marked directly on the packaging. Instead, the variable information is written on a label.
Often used here thermotransfer.
The technology is based on transferring ink from an ink ribbon to the label using heat. The result is very high contrast and extremely sharp prints.
Small labels require high precision
When the label is only a few centimeters wide, there is no room for blurry characters. This is especially true on small vials and ampoules where the label must contain the product name, batch number, serial number and sometimes even a Datamatrix code.
The smaller the label, the higher the demands placed on both the printer and the label material. Here is a detail that is often overlooked. It doesn't matter how good the printer is if the label has the wrong surface texture. A rough paper label limits how small details can be reproduced.
If you want to print very small characters, you will need a smooth label material, often plastic, where the color can be reproduced with maximum precision. It is the interaction between printer and label material that determines the end result.
Laser – permanent marking with high demands on the material
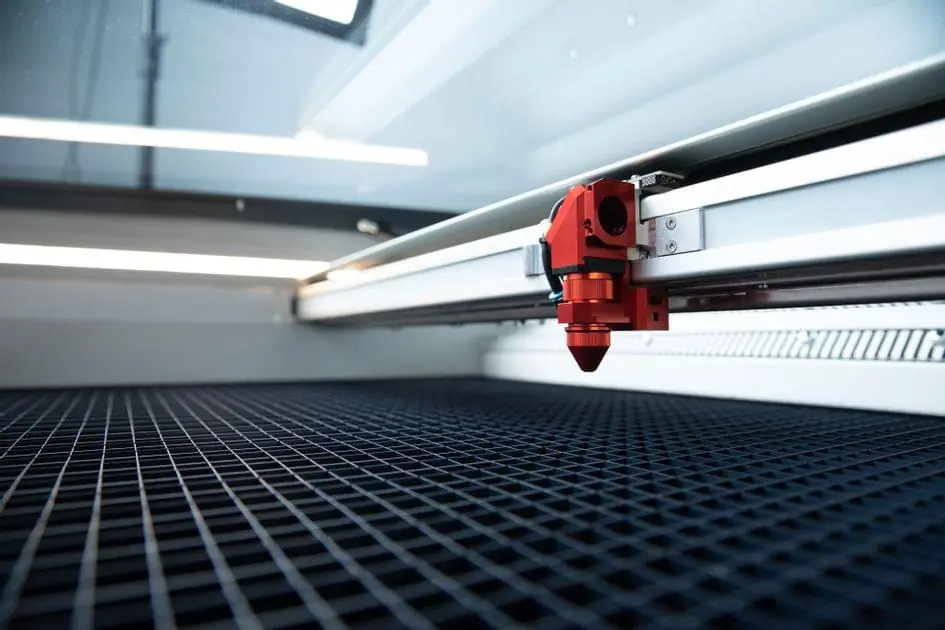
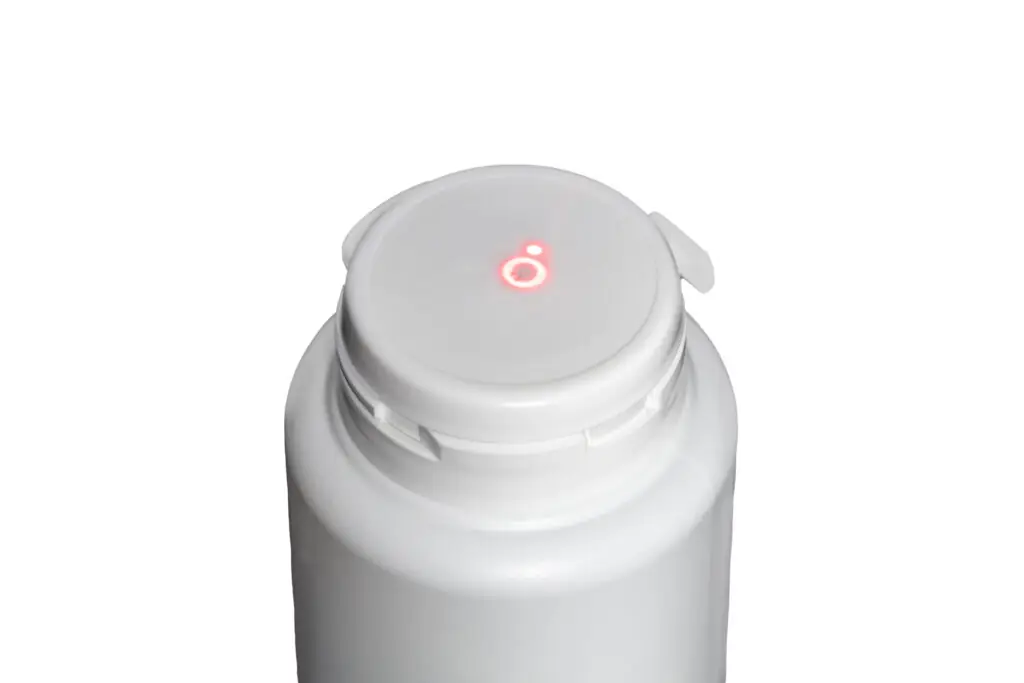
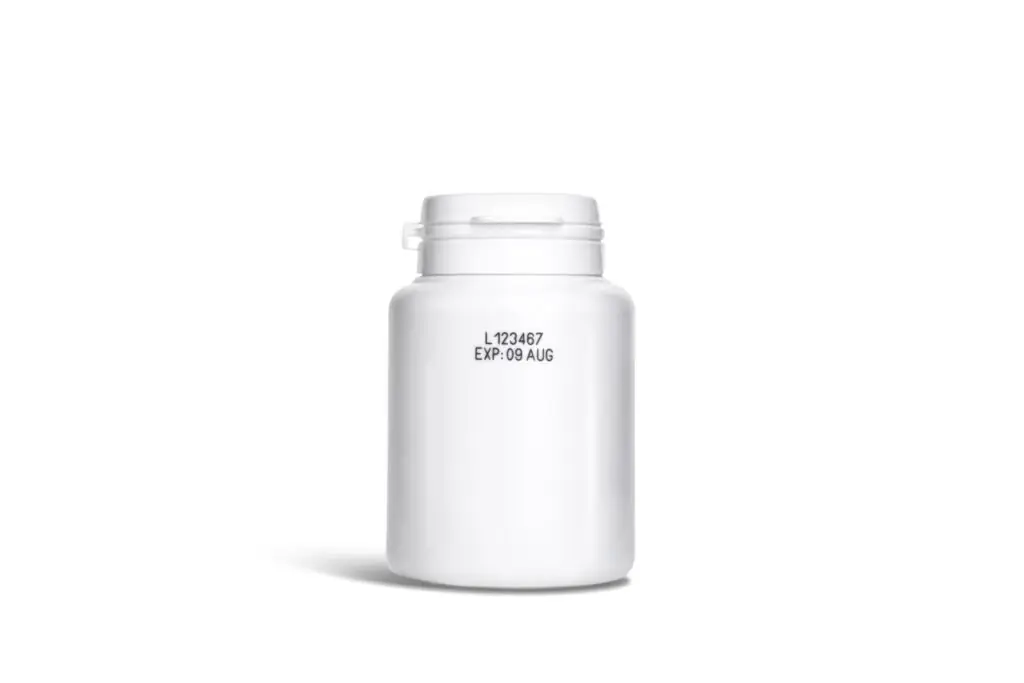
Laser marking is often described as the most maintenance-free marking technology, and to some extent that is true. Since the technology does not use ink or cartridges, the need for consumables is eliminated.
This means fewer downtimes and low running costs. But in the pharmaceutical industry, the choice is much more complex than that.
Permanent does not mean automatically approved
The great strength of laser is that the marking is permanent. The text cannot be washed off or faded in the same way as ink. But that does not automatically mean that it meets the requirements of the pharmaceutical industry. For a Datamatrix code to be approved, it is not just a matter of its presence.
It must also have the right contrast. It must be verifiable. It must be readable by vision cameras. It must meet the right quality class.
If the laser provides too low contrast, it doesn't help that the marking is permanent. It can still be rejected. That's why material tests are almost always carried out before laser is chosen as a marking technology.
The material determines whether laser is the right choice
Different plastics react differently. Different glasses react differently. Cardboard reacts differently. Even two materials that look identical can produce completely different results when marked with a laser.
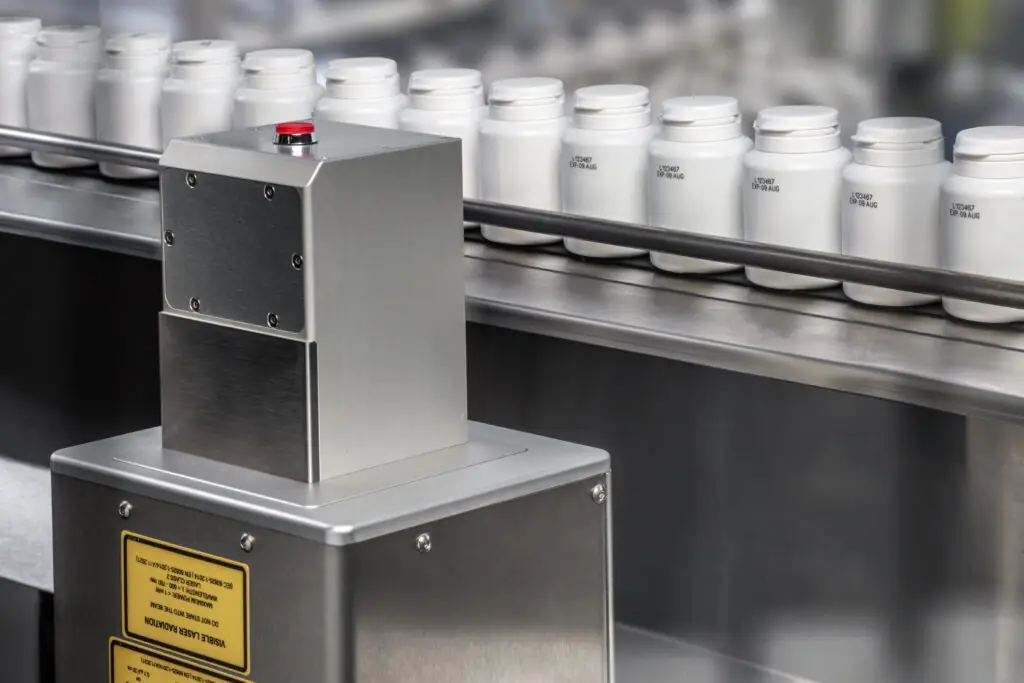
That's why many projects begin with extensive testing where different laser powers, speeds and wavelengths are tried until the combination that provides the right contrast and readability is found.
Only then can you determine whether laser is truly the optimal solution.
The technology is always chosen based on the overall picture.
A common misconception is that the choice of marking technology is made based on the printer itself. In practice, the printer is only part of the system. When designing a marking solution, the entire production process is instead analyzed:
- What does the product flow look like?
- How fast does the line go?
- What does the product look like?
- What material is it made of?
- How large is the marking area?
- What information should be written?
- Should the information be verifiable by machine?
- What does the subsequent process look like?
- Should the product be sterilized, refrigerated or exposed to chemicals?
- How will the label be readable in five years?
Only when all these questions are answered can it be determined which technology provides the most reliable and future-proof solution.
This is also why two pharmaceutical products that at first glance look almost identical may require two completely different labeling systems.
Vision cameras and verification systems – why a readable code is not always an approved code
Many people associate vision cameras with simple quality control. They imagine a camera that photographs the product and determines whether the barcode can be read.
In reality, modern vision system considerably more advanced than that.
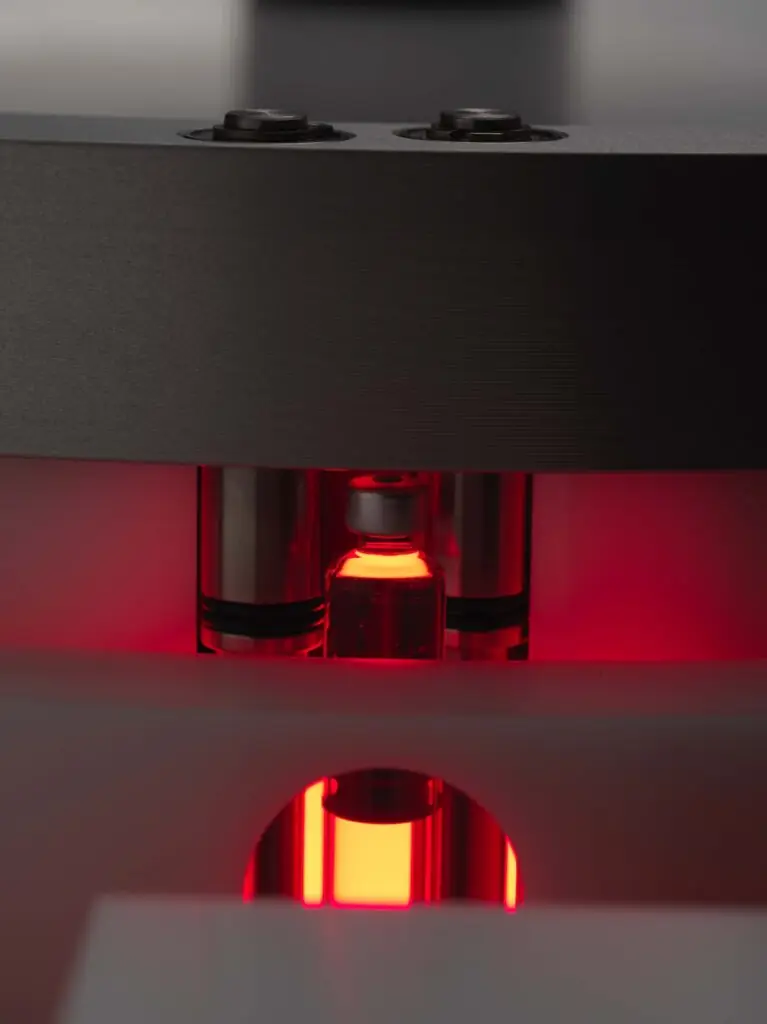
In the pharmaceutical industry, the vision camera functions as an integral part of the production line's quality assurance. Its task is not only to check that a label is present, but to ensure that the right information has been written on the right product, in the right place and with sufficient quality to meet both regulatory requirements and the company's internal quality requirements.
In many production lines, the vision camera is also the final control point before the product is allowed to leave the labeling station.
A camera doesn't just look for a Datamatrix code
It's easy to think that a vision camera only checks whether a Datamatrix code or barcode can be read. That's only a small part of its work.
A modern vision system can simultaneously control:
- that the right product is in the right production flow
- that the marking is in the correct position
- that the text has the correct orientation
- that the batch number and expiration date match the production order
- that serial numbers have not been duplicated
- that the Datamatrix code is of the correct quality
- that the label is straight and not wrinkled
- that the label is not missing
- that safety labels have been applied correctly
- that the packaging has not been damaged during the process
In practice, this means that the camera becomes part of the production line's decision-making. If something deviates, the product is automatically stopped or directed to a separate reject path for further inspection.
It's not enough that the code is readable
One of the most common misconceptions in industrial marking is that a code is approved as long as it can be read with a streckkodsläsare.
This is not how it works in the pharmaceutical industry. A Datamatrix code can be fully readable by a hand scanner but still be rejected by a verification system.
The reason is that the verification assesses significantly more parameters than readability itself. Examples of factors that are analyzed are:
- contrast between code and background
- the size and shape of the modules
- edge definition
- print quality
- damage or deformations
- Quiet Zones around the code
- the geometric structure of the code
If any of these parameters fall outside the tolerances, there is a risk that the code will not be able to be read as reliably further down the distribution chain.
The pharmaceutical industry therefore not only accepts that the code works today – it should work just as well after transportation, storage and handling.
Verification is about quality – not just function
To measure the quality, special code verifiers are used according to international standards, such as GS1. A verifier does not work in the same way as a regular barcode reader. A barcode reader tries to read the information. A verifier instead analyzes how good the code actually isIt provides a quality result where parameters such as contrast, module size, sharpness and geometric accuracy are weighed together.
This allows quality issues to be detected long before they become production issues, making verification an important tool for validating the labeling process and for recurring quality checks.
The camera may not verify itself.
One detail that is often overlooked is how the information is checked. It is not enough for a camera to read the text and determine that it contains, for example, a batch number. 12345.
What happens if the wrong batch number was sent to the printer initially?
Then the camera will still read 12345 and approve the labeling, even though the product should actually have been labeled with a different number. That is why many pharmaceutical manufacturers work with multiple levels of control.
The vision system compares the printed information with data from a higher-level system, such as a recipe system, an MES system or a database. The camera therefore not only checks what is written on the productIt checks that it is exactly the information that should have been there.
This is often described as a “handshake” between systems and is an important part of a modern quality assurance system. By comparing multiple independent sources of information, the risk of an incorrect recipe or operator error leading to mislabeled products is reduced.
The vision camera is just one part of a larger quality system
In a modern pharmaceutical line, the camera does not work alone. It communicates continuously with:
- the printer
- The PLC system
- HMI panel
- recipe database
- The MES system
- serialization system
- the reject system
Each component has its task. The printer produces the marking. The vision camera checks the result. The PLC controls the product flow. The MES system delivers product data. The Reject system sorts out faulty products.
Together they form a closed quality system where each component verifies the next step in the process.
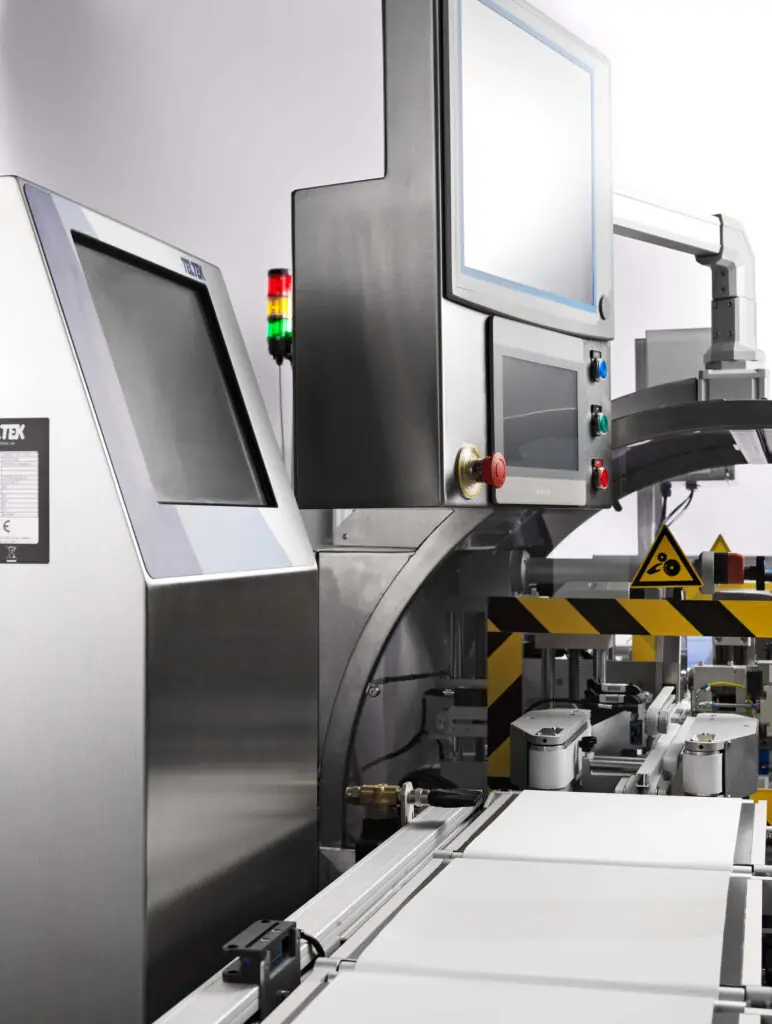
The Reject system – the final safety barrier
When a product is rejected by the vision camera, it is not allowed to continue to the next process step. Instead, a reject system is activated. Depending on the design of the production line, this can consist of:
- a pneumatic ejector
- a servo-controlled arm
- an air nozzle
- a separate transport lane
- a collection container for non-conforming products
The important thing is that only approved products are allowed to continue.
The reject system also often documents why the product was rejected, making it possible to analyze recurring errors and identify the cause before the problem affects production on a larger scale.
Transparent products require completely different sensors
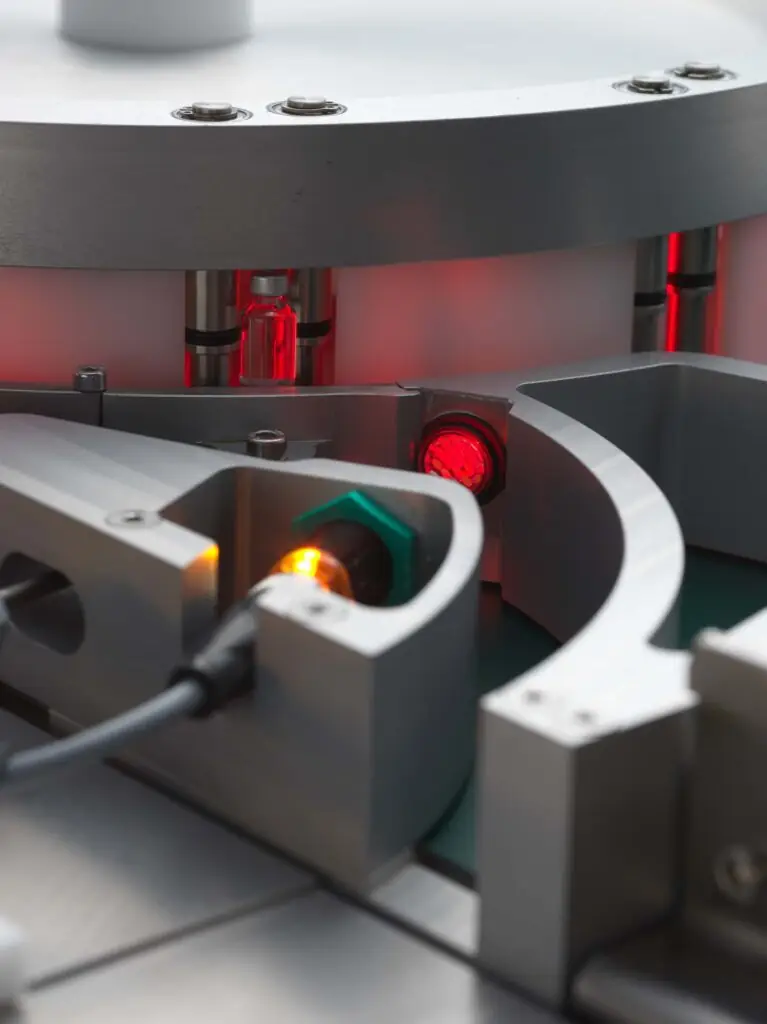
The pharmaceutical industry works extensively with glass bottles, vials and transparent plastic containers, which poses major challenges for standard optical sensors.
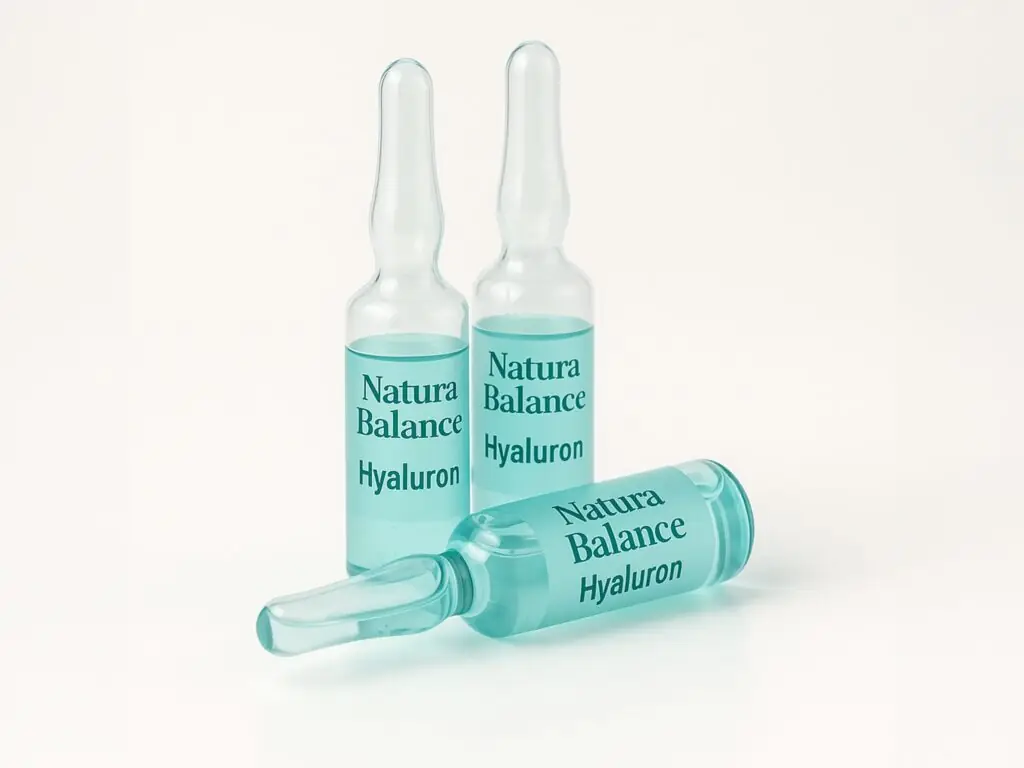
A traditional photocell often has difficulty determining whether a transparent product is actually passing in front of the sensor. Therefore, specially adapted sensors are used instead.
For example:
- ultrasonic transducer
- photocells with reflector mirror
- sensors for transparent materials
- laser sensors with background suppression
The technology used is determined by the product's material, shape and speed.
Even transparent labels can be checked
Another challenge is transparent labels. For the consumer, they provide an exclusive and discreet appearance. For a vision system, however, they pose significantly greater demands.
To inspect a transparent label, special lighting or a bright background behind the product is often used. This allows the camera to clearly distinguish the label from the transparent packaging.
In some applications, UV fluorescent markings are also used, which are only visible under specific lighting. This can be used both for quality control and as an additional security feature against counterfeiting.
The sensor choice affects the entire machine design
When designing a marking solution, the sensor is rarely a detail that is chosen at the end of the project. On the contrary. The sensors are often crucial to how the entire machine is built. Should the product be detected from the side? From above? Against a reflector? Does it need to be rotated before marking? How does ambient lighting affect the result?
All of these questions need to be answered during the design phase, which is why two seemingly similar pharmaceutical products can require completely different sensor solutions.
Vision does not replace the operator – it complements the human
Despite today's advanced automation solutions, the operator still plays an important role. The difference is that modern production lines are designed to reduce the dependence on the human factor. The operator should not have to detect every error with the naked eye.
Instead, vision cameras, verification systems and digital controls are used to identify deviations much earlier and with significantly higher precision than is possible manually.
This not only means higher quality, it also creates a more repeatable production where the same high labeling quality can be maintained across millions of products.
When quality assurance is built on multiple levels – from prescription control and vision control to verification and automatic sorting – a robust process is created where the probability of a mislabeled product reaching the market becomes very small. It is precisely this systems thinking that characterizes modern labeling solutions in the pharmaceutical industry.
From individual packaging to finished pallet – this is how traceability works in practice
A pharmaceutical package is rarely a stand-alone product. It is part of a much larger information flow.
When a product leaves the labeling station, it has already been given a digital identity that follows it through the rest of the distribution chain. That identity is as important as the medicine itself in the packaging.
To understand how modern pharmaceutical labeling works, you therefore need to look at the entire production chain – not just the individual printer or the labeling machine.
Serialization – each individual product gets a unique identity
Since the introduction of the EU's Falsified Medicines Directive (FMD), serialization has become an inherent part of pharmaceutical production. The principle is simple.
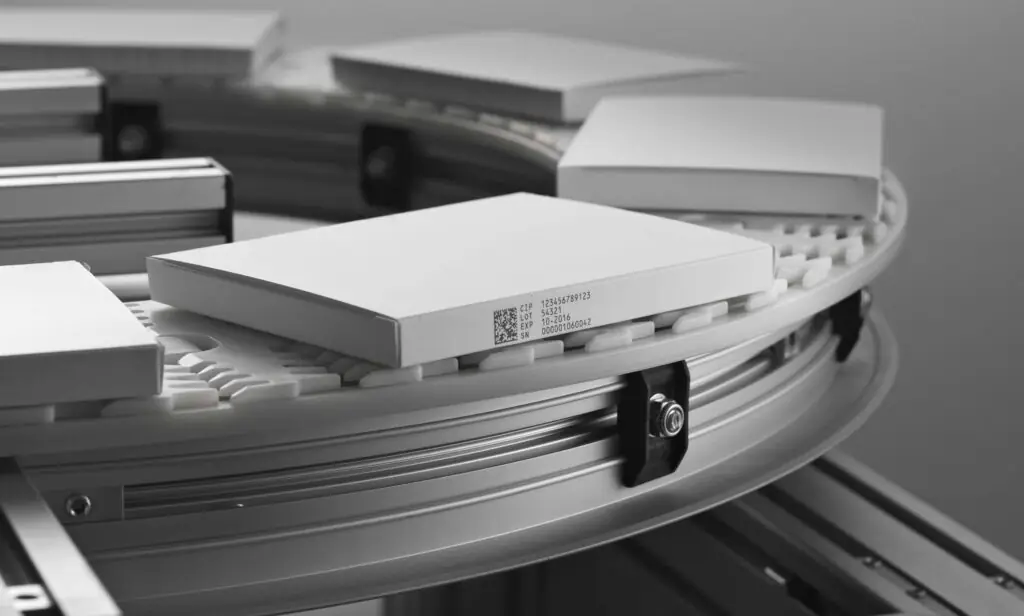
Each individual medicine package is assigned a unique serial number that is never reused. The serial number is usually combined with:
- GTIN
- batch number
- expiration date
The information is encoded in a Datamatrix code and stored simultaneously in the manufacturer's system, meaning that each individual carton can be individually identified throughout the distribution chain.
When the medicine leaves the factory, there is therefore a digital connection between the physical product and the information that describes it.
Aggregation – the next step in traceability
But the work doesn't end when the carton is labeled. When multiple pharmaceutical packages are packed into a shipping carton, the next level of traceability is created. The system records exactly which serial numbers are in the carton in question.
When multiple shipping cartons are then placed on a pallet, another connection is created. Now the system knows:
- what products are in each carton
- which cartons are on the pallet
- which pallet ID belongs to the delivery
This is usually called aggregation.
The result is a digital hierarchy where you can follow a product from individual packaging all the way up to pallet level – or vice versa. If an individual serial number is scanned, it is possible to see which carton and which pallet the product belonged to. Similarly, an entire pallet can be identified without having to scan each individual packaging.
Why aggregation is so important
Aggregation is not just about logistics. It is a crucial part of the pharmaceutical industry's safety work.
If a discrepancy is detected, the manufacturer can quickly identify:
- which products are included in the current batch
- which boxes they are in
- which pallets contain these cartons
- which wholesalers received the delivery
- which products are still in the distribution chain
This makes recalls significantly faster and more accurate than before. Instead of recalling entire production runs, it is often possible to limit the recall to exactly the products affected.
Labeling is about more than applying a label
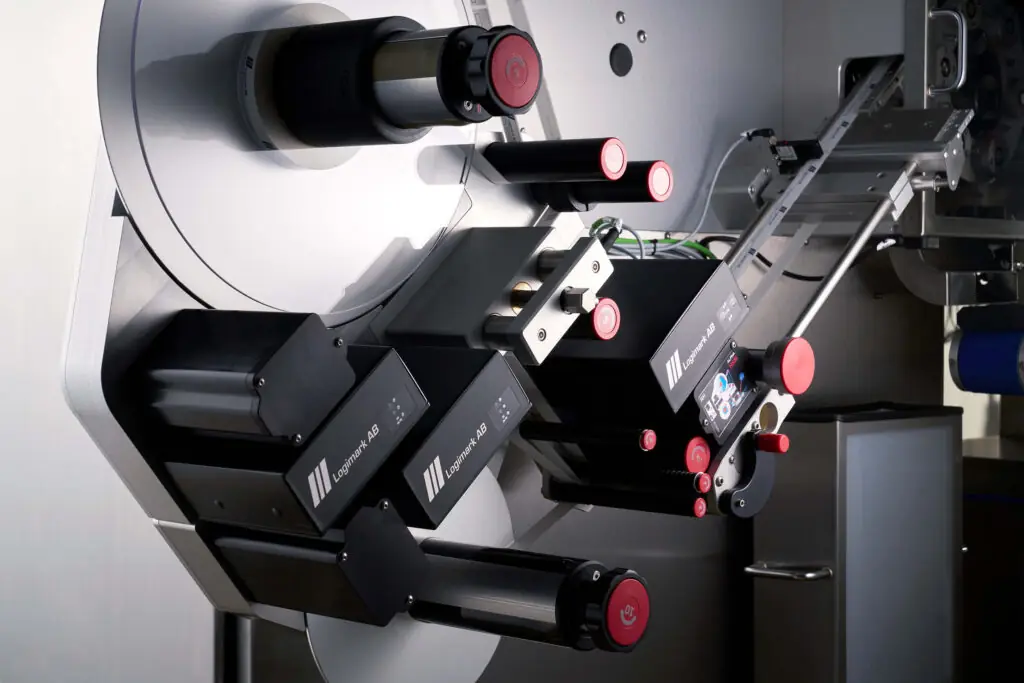
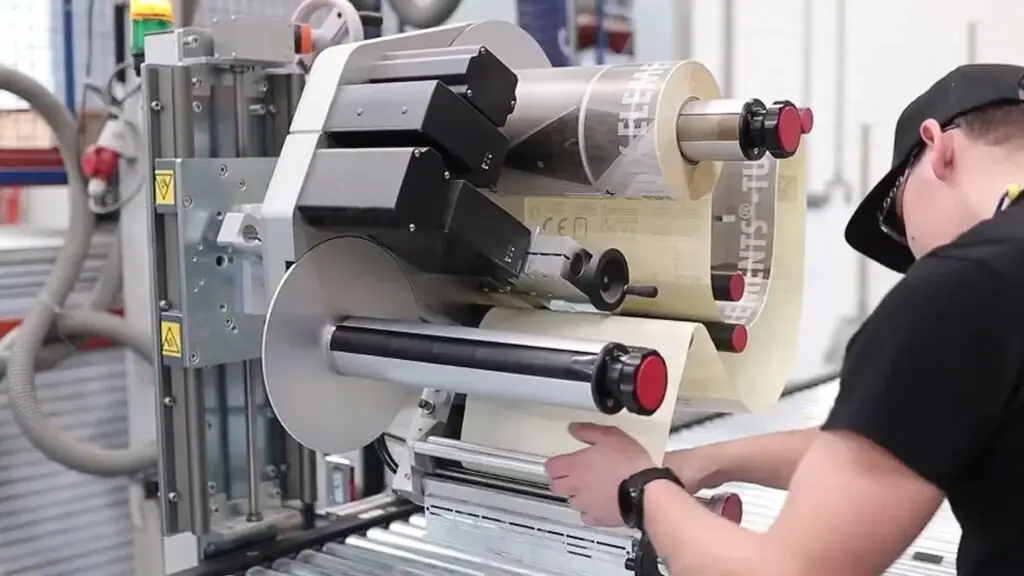
Many people associate labeling with a simple label applicatorIn the pharmaceutical industry, the reality is significantly more advanced.
A label can simultaneously function as:
- information carrier
- identification marking
- security seal
- traceability carrier
- tamper protection
In addition, the same product may need several different labels.
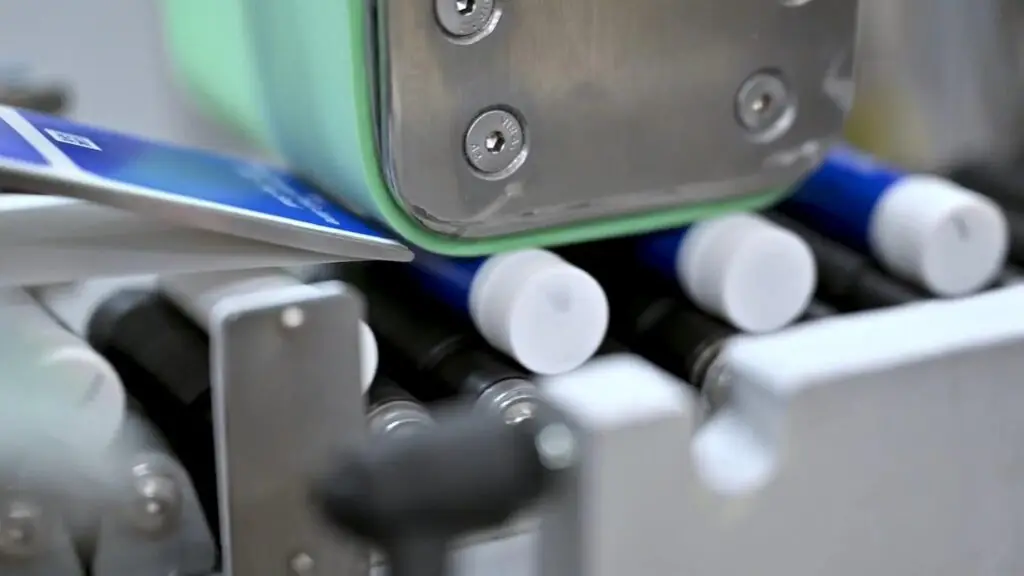
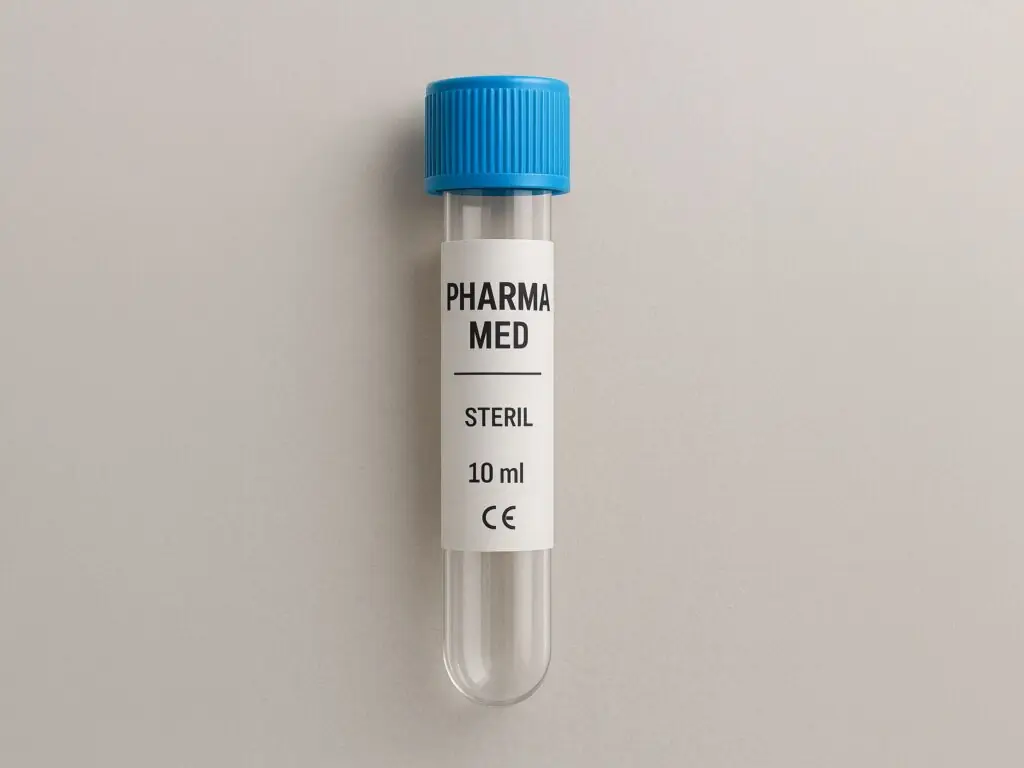
For example:
- front label
- back label
- neck label
- security label
- logistics label
Each label must be applied with high precision and then verified before the product is allowed to continue through the production line.
Security labels reveal tampering
Many pharmaceutical packaging uses special safety labels, so-called Tamper Evident-labels. Their job is not just to keep the packaging closed. They should clearly show if someone has tried to open the product. That's why they are designed to be permanently altered when broken.
Some leave a VOID pattern. Others crack. Still others are perforated so that they cannot be restored once broken.
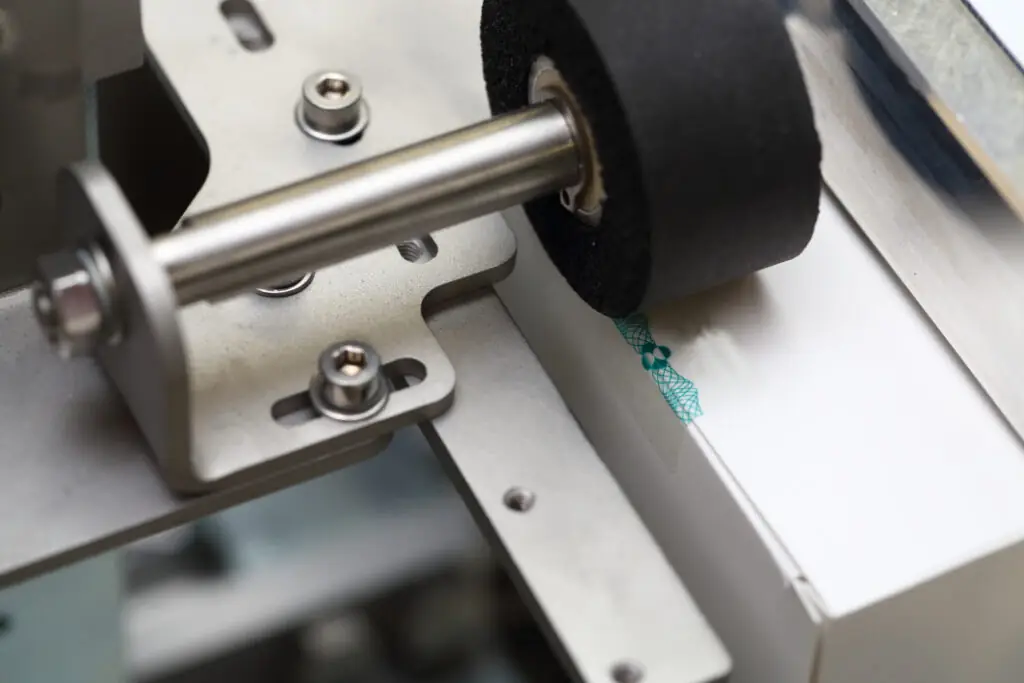
What they have in common is that they should make it impossible to open the packaging without the manipulation becoming visible.
Multiple labels require a coordinated labeling process
It is not uncommon for a pharmaceutical product to need several different labels applied during the same production flow.
It could be, for example:
- product label
- batch label
- security label
- logistics marking
In some production lines this is done in several separate stations. In others, combined labeling machines where multiple label units work in sync. The advantage of an integrated solution is that all labels are applied under the same control system.
This means that:
- prescription changes are made centrally
- all labels are checked by the same vision system
- product data is retrieved from the same data source
- the risk of operator error is reduced
Recipe management reduces the risk of human error
One of the most common causes of mislabeling is not that the printer makes a mistake. It's that the wrong information is sent to the printer. That's why modern pharmaceutical lines are increasingly working with prescription management.
The operator selects the relevant product in the HMI system. The system then automatically loads:
- correct layout
- correct etiquette
- correct product information
- correct batch structure
- correct serialization data
The operator does not need to manually enter the information. This reduces the risk of errors and also makes product changes significantly faster.
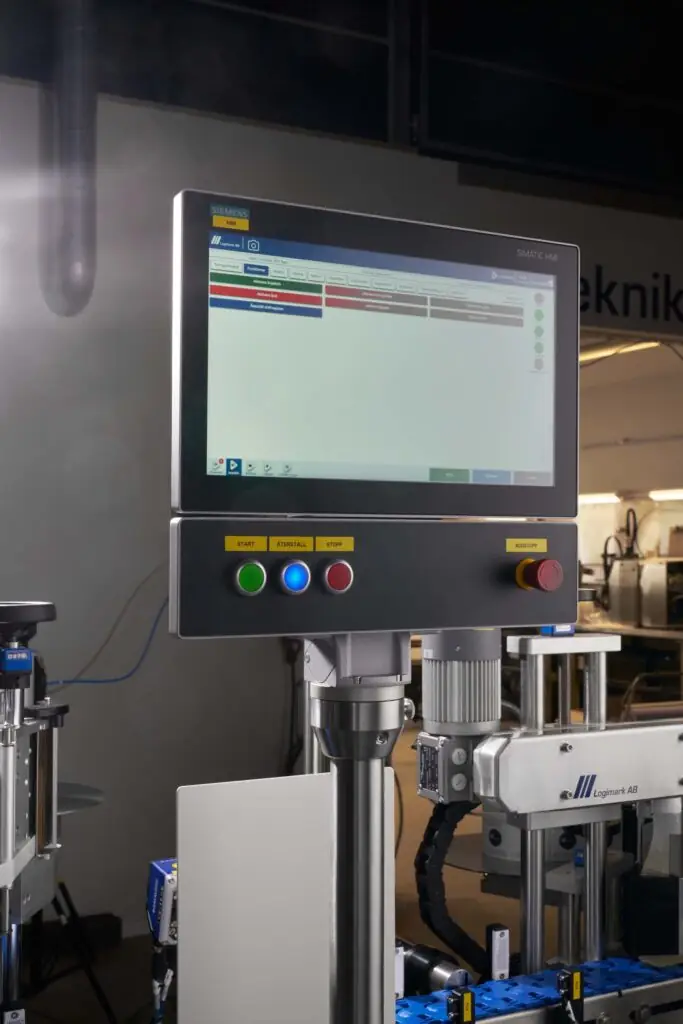
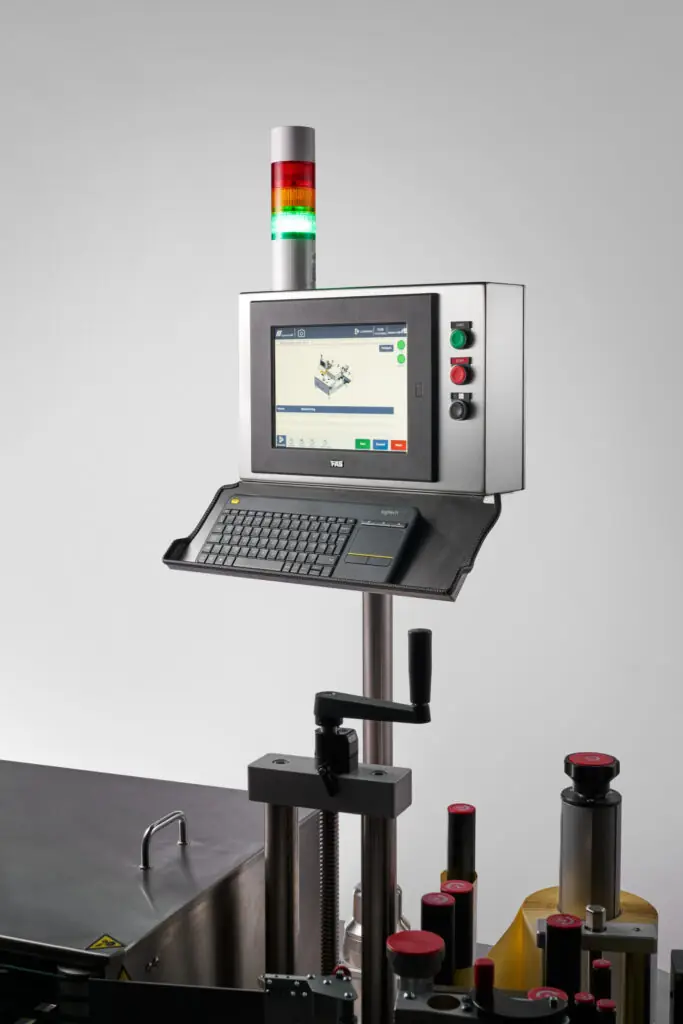
At many pharmaceutical facilities, this is combined with requirements for double approval, where two people must verify the product change before production can begin.
An HMI becomes the hub of the entire labeling system
In modern labeling lines, the HMI panel is much more than a start and stop button.
It acts as the operator's control center.
From here you can, among other things:
- choose product recipe
- supervise production
- see alarm history
- follow statistics
- control vision cameras
- manage user permissions
- carry out product replacements
When the entire labeling line is controlled from a common HMI, production becomes both simpler and safer. The operator does not have to work in several different systems at the same time, which reduces the risk of incorrect settings.
Automation is about much more than higher capacity
When talking about automation, it's easy to focus on increased production rates. In the pharmaceutical industry, the biggest gain is often something completely different. Automation creates repeatability.
This means:
- more consistent quality
- fewer operator-dependent moments
- better documentation
- higher traceability
- easier validation
- less risk of human error
This is also why many pharmaceutical companies are gradually automating steps that were previously performed manually, for example labeling, carton erecting, sealing and logistics marking.
The future of pharmaceutical labeling is becoming increasingly digital
Development is happening rapidly. Vision cameras are becoming more intelligent. Data volumes are increasing. Integration between machines and business systems is becoming tighter.
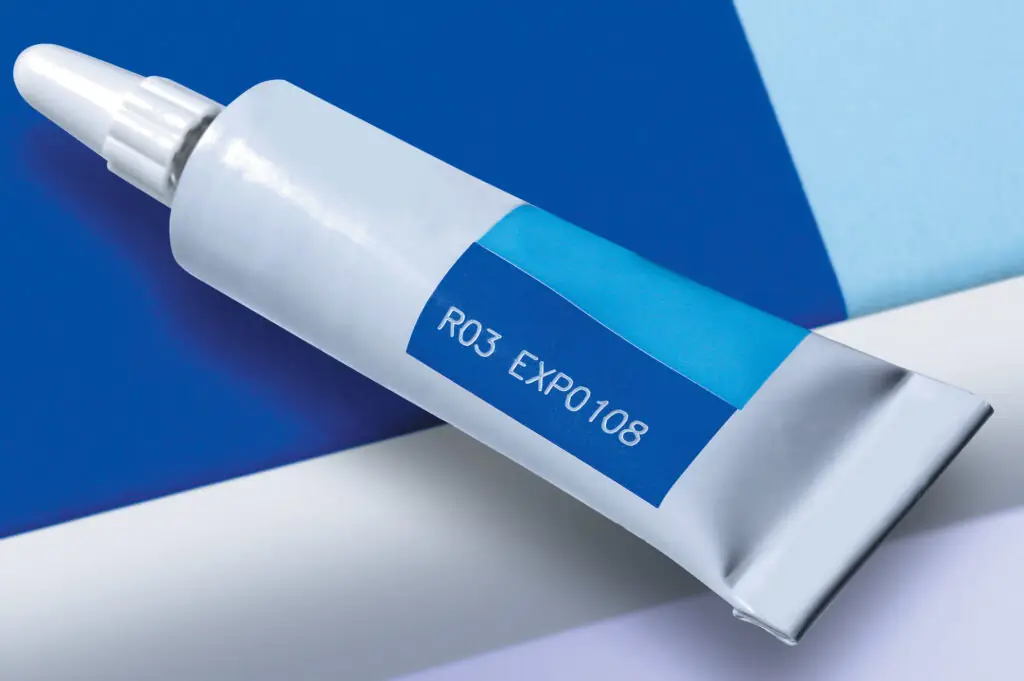
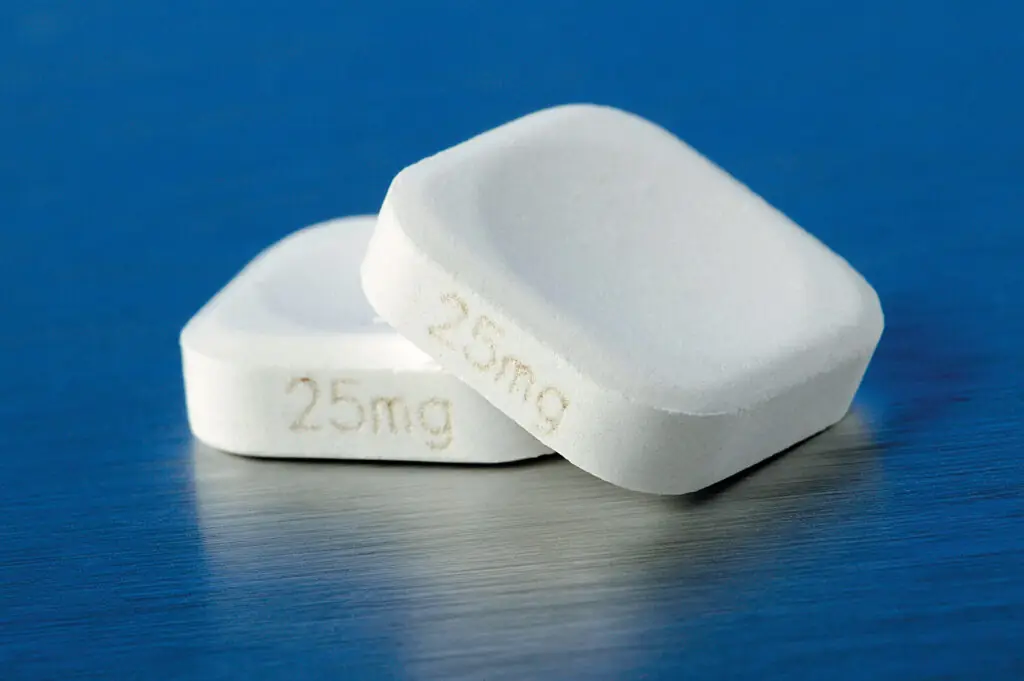
At the same time, the use of digital product information is increasing. QR codes and Datamatrix codes are no longer used solely for traceability. They can also provide access to:
- digital package inserts
- instructions for use
- safety information
- product updates
- language versions
- verification of product authenticity
This means that the amount of printed information on the packaging itself can be reduced while at the same time increasing access to current information.
AI will primarily strengthen quality control
There is a lot of talk about artificial intelligence in the industry. When it comes to labeling itself, the areas of application are still relatively limited.
However, there is great potential in quality control. Future AI-based vision systems will likely be able to identify deviations that are currently difficult to detect with traditional image processing.
For example, AI can be used to:
- detect subtle typos
- identify changes in print quality before they become critical
- analyze recurring production errors
- optimize maintenance of printers and labeling equipment
- predict component failures before they cause production downtime
AI will therefore likely act as a complement to today's verification systems rather than replacing them.
Summary – a modern labeling solution is a complete quality system
It's easy to see labeling as the last step before a product leaves the factory. In reality, it's one of the most integral parts of the entire production process.
A modern labeling solution does not just consist of a printer or a labeling machine. It involves an interaction between:
- marking technology
- labeling
- vision cameras
- sensors
- PLC system
- HMI
- recipe control
- serialization
- aggregation
- verification
- quality documentation
Each component has a clear task, but it is only when they work together that the high level of safety that the pharmaceutical industry requires can be achieved.
For the manufacturer, this not only means that legal requirements are met. It also creates stable and repeatable production where each individual product can be identified, verified and tracked throughout its entire life cycle – from the first labeling in the factory to the finished pharmaceutical package at the patient's bedside.